Static Electricity: The Small Charge Behind Costly Quality Problems
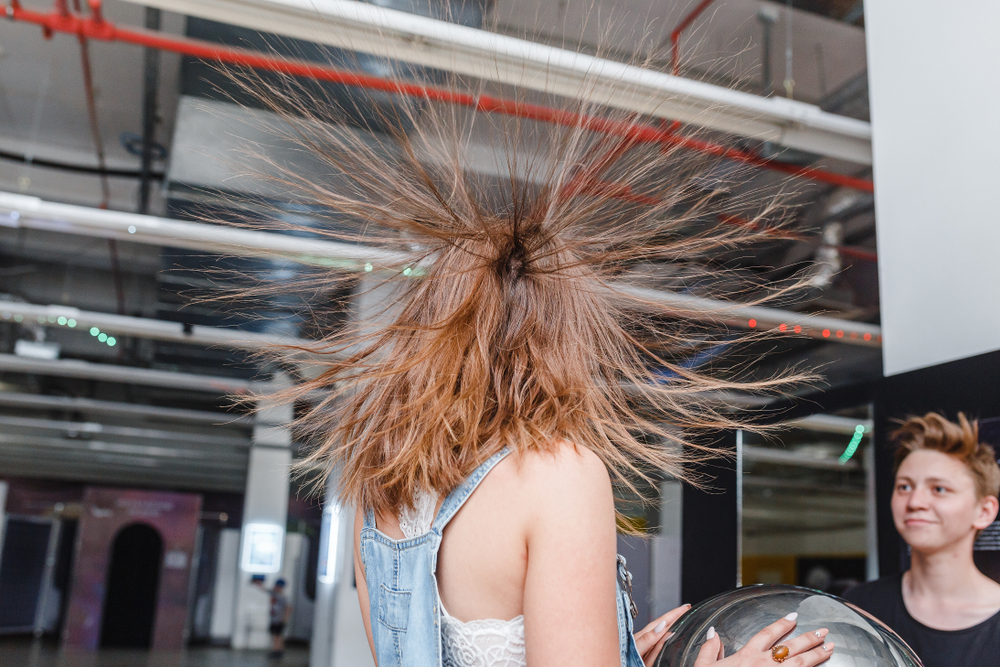
Static never appears as a line on the profit and loss account. In packaging, printing, plastics and electronics, it still shows up every day as rejects, slow lines and customer complaints.
A charge nobody can see makes dust cling to a part, film stick to itself, sheets misfeed and labels lift. Because the symptoms look like a dust problem or a handling problem, the cause often goes unnamed, and the cost is spread across scrap, labor and downtime.
Where static comes from
Static builds when materials rub, slide or separate: film unwinding from a roll, a plastic part leaving a mold, sheets moving along a conveyor, a bottle brushing a guide rail. Plastics and other insulating materials hold that charge because it has nowhere to drain. Dry air makes it worse, which is why many plants see static problems rise in winter, when heating lowers indoor humidity.
Who feels it most
Almost any plant that handles plastics, films or paper deals with static at some point, but a few sectors feel it more than most. Packaging lines see film that refuses to open and labels that lift before they are applied. Printers lose time to sheets that double-feed or stick in the delivery. Molders and extruders find dust on parts that are about to be painted or assembled. Electronics assemblers worry less about dust and more about the discharge itself, which can damage components without leaving any visible sign. Paint and coating lines see the result as small specks under the finish that send a part back for rework.
What it costs the business
- Contamination. A charged surface pulls dust out of the air and holds it. Before painting, coating, printing or filling, that dust becomes a defect.
- Handling faults. Films cling, sheets stick together, and light parts jump, jam or fall off the line.
- Safety and equipment. Discharges give operators shocks and can damage sensitive electronics. Where flammable solvents or dusts are present, a spark is an ignition risk.
- Hidden labor. Operators wipe parts by hand, slow the line, or rerun jobs, and that time is rarely booked to static.
Why blowing the dust off is not enough
The usual first response is to blow the dust away with compressed air. On a charged surface, that often disappoints. The charge holds the particles in place, and moving air does nothing to remove the charge, so the surface starts collecting dust again as soon as the air stops.
Neutralize and clean in one step
Ionizers solve the underlying problem. They produce positive and negative ions that drift onto a charged surface and cancel the charge, so the dust lets go. Pair that with airflow and both jobs happen together: an ionizing air knife carries ions to the surface on a sheet of air, neutralizing the charge while the air carries the loosened dust away. On a moving line, this happens in a single pass with no contact.
Other tools have their place too. Ionizing bars suit thin webs and films with little dust. Ionizing nozzles and guns handle spot cleaning. Grounding and humidity control work in the background to reduce how much charge builds in the first place.
Four questions for operations leaders
- Where do the rejects cluster? Dust defects that follow a particular unwind, mold or conveyor point usually lead straight to the source.
- When do problems peak? A seasonal pattern points to humidity.
- Is the current fix maintained? Ionizers need regular cleaning and checking to keep working.
- What does the workaround cost? Count the wipe-downs, slowdowns and reruns, not only the scrap.
A small fix with an outsized return
Static is cheap to measure. A handheld static meter shows where the charge is and how strong it is. Start at the station with the most dust-related rejects, measure before and after a change, and let those numbers make the case for the rest of the plant.