The Welding Ventilation Paper Trail: What Facility Managers Should Document Before an Inspection
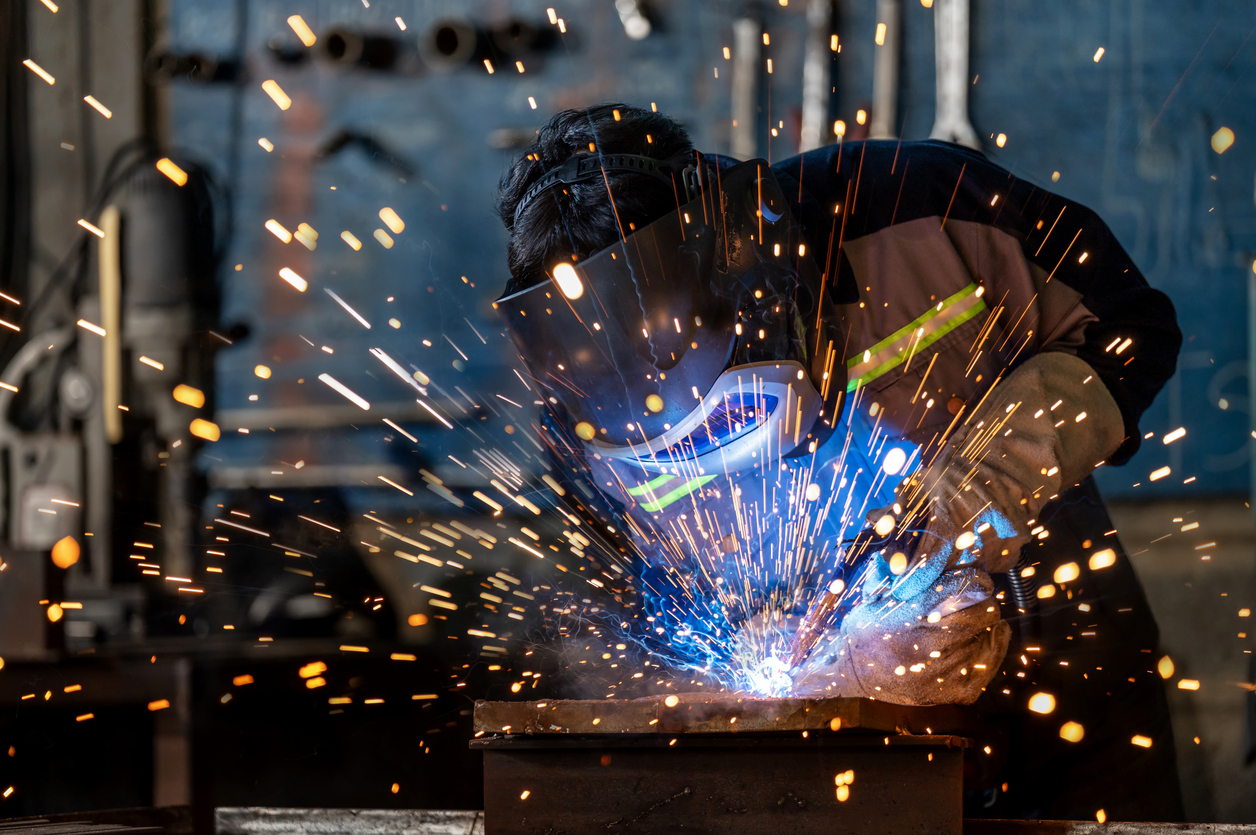
Most welding shops install extraction equipment and assume the job is finished, then struggle to show an inspector, insurer, or auditor what that equipment actually does. A system that works on the floor but cannot be demonstrated on paper leaves a real gap. Facility managers who read a breakdown of OSHA welding ventilation requirements usually find that the standards expect more than hardware: they expect a shop to understand its hazards, apply controls, and keep those controls working. This post covers the documentation that closes that gap.
Key Takeaways
- Ventilation records matter as much as the extraction equipment itself, because undocumented controls are hard to defend.
- A hazard map, a capture verification routine, and a maintenance log form the core of a defensible paper trail.
- Documentation should change when the work changes: new base metals, new processes, or a new bay layout all trigger a review.
- Good records also help the shop, since they expose weak capture and overdue filters before workers feel the effects.
Why It Matters
Welding fume is a mixture of fine particulates and gases, and its makeup depends on the base metal, filler, coating, and process. Mild steel, stainless, and galvanized work each produce a different exposure profile. A shop that treats all of it as "general smoke" will under-control some jobs and overspend on others.
Inspections, insurance reviews, and customer audits increasingly ask for evidence rather than assurances. Saying "we have extractors" is a statement. Showing where they sit, what they capture, how often filters change, and when airflow was last checked is a record.
There is also an operational payoff. Shops that keep ventilation logs catch declining performance early, which reduces unplanned downtime and keeps weld quality steadier. Documentation supports compliance efforts, but it never replaces the controls themselves, and no paperwork can guarantee a particular regulatory outcome.
What a Defensible Ventilation Record Actually Contains
A defensible ventilation record answers four questions: what are the hazards, what controls address them, how do you know the controls work, and who keeps them working. Each answer should live in a document that a new supervisor could pick up and understand without a walkthrough.
The table below summarizes the core records and what each one proves.
Notice that none of these records are complicated. Their value comes from being current, specific, and tied to named stations rather than the shop in general.
Step One: Build a Hazard Map by Station
A hazard map lists every welding station, the metals and processes used there, and the fume constituents that result. Start with a simple floor plan and annotate it by station number.
Capture the Variables That Change Fume Composition
Record the base metal, filler wire or rod, any coatings or platings, and the process (MIG, TIG, stick, flux-core). Flux-core and stick typically generate heavier fume loads than TIG, and coated or plated material introduces additional concerns. Stainless work raises hexavalent chromium questions, while mild steel brings manganese exposure into focus.
Note Who Works Nearby
Fume does not respect station boundaries. Mark adjacent grinding, assembly, and inspection areas, since workers there share the same air. This is where many shops discover that the people with the least protection are not the welders at all.
Pro Tip: Walk the floor with the hazard map during a normal production shift, not a quiet one. Stations that look fine at half load often reveal capture problems at full load.
Step Two: Verify Capture, Not Just Airflow
Capture verification confirms that fume is drawn away from the breathing zone, which is a different question from whether a fan is running. An extractor can move plenty of air and still miss the plume if the arm sits too far from the arc.
Simple Checks That Produce Useful Notes
Shops can run a visual smoke or fume-plume observation at each station, noting whether the plume is drawn into the hood or drifts past it. Record the hood distance from the arc, since capture drops off quickly as that distance grows. Where airflow instruments are available, log hood face velocity and compare it to the equipment's rated performance.
Match Equipment to the Task
Portable units suit changing work locations, while fixed or ducted systems suit repeat, high-volume stations. Teams exploring portable and industrial-grade welding fume extraction equipment can use their hazard map to decide where each type belongs. Whichever format a shop chooses, the verification routine should be written down and repeated.
Step Three: Keep a Maintenance and Filter Log
A maintenance log records every filter change, fan inspection, and duct check with a date, a station or unit ID, and a name. Loaded filters raise resistance, cut airflow, and quietly erode capture long before anyone notices smoke in the bay.
What to Log Every Time
- Unit or station identifier
- Date and operator or technician name
- Filter type and condition found
- Pressure drop or airflow reading, if the unit provides one
- Any corrective action taken
Set Triggers, Not Just Calendar Dates
Calendar schedules work as a floor, but production volume drives filter loading. Add triggers such as a pressure-drop threshold, a visible drop in capture, or a sustained increase in shift hours. A log that shows changes made because of a trigger demonstrates active management rather than box-checking.
Step Four: Tie Training and Change Control to the Records
Operator technique is the most variable part of any extraction system, so training should be documented alongside the hardware. Positioning an arm or hood correctly takes seconds, and skipping it takes the benefit away.
Add a short change-control rule: whenever a shop adds a new base metal, a new process, a new bay, or a new extractor, someone must update the hazard map and re-verify capture at the affected stations. Without that rule, records drift out of date within months and lose their value.
Key Insight: Outdated documentation can be worse than none. It shows that a shop knew a control mattered and then stopped checking it.
Example: A Mid-Size Fabrication Shop Rebuilds Its Records
Consider a fabrication shop with eight welding stations, a mix of mild steel and occasional stainless work, and a combination of fixed and portable extractors. The shop owner had equipment invoices but no station-level records. When a customer audit asked how the shop controlled stainless welding fume, nobody could answer with specifics.
The safety lead spent one week building the paper trail. She mapped each station by metal and process, flagged the two stations that handled stainless, and ran plume observations at all eight. Three stations showed weak capture because the arms were routinely parked too far from the arc.
The team repositioned the arms, added a hood-distance mark on each one, and started a shared filter log. Within a month the log showed that one unit loaded far faster than the others because it served the highest-volume station. The shop moved that unit to a shorter change interval and added a pressure-drop trigger. At the next customer audit, the lead handed over a hazard map, verification notes, and a maintenance log in a single folder.
The point is not that paperwork solved the problem. The exercise of building the records exposed three real capture problems and one mismatched service interval.
Actionable Takeaways
- Draw the hazard map this month. List every station with its metal, process, and coating, and mark adjacent work areas.
- Run a plume check at each station during full production. Note hood distance and whether fume is drawn into the capture zone.
- Start a single maintenance log. Include unit ID, date, filter condition, and the name of whoever did the work.
- Add change-control triggers. New metal, new process, or new layout means an update to the map and a fresh capture check.
- Document operator training. Keep sign-offs on positioning and use, and refresh them annually.
- Review the full folder quarterly. Remove stale entries and confirm every station still matches reality.
Conclusion
A welding ventilation program is only as strong as the evidence that it works. Hazard maps, capture notes, and maintenance logs cost little to build, and they turn an equipment purchase into a managed control. Shops that keep them current find problems sooner and answer audit questions with confidence, while keeping attention on the real goal: cleaner air for the people doing the work.
FAQ
What records should a welding shop keep for ventilation?
A welding shop should keep a station-level hazard map, an equipment inventory, capture verification notes, a filter and maintenance log, and training sign-offs. Together these show which hazards exist, which controls address them, and that the controls are maintained.
How often should welding fume extraction be checked?
Capture should be checked at least monthly and after any change to layout, process, or base metal. High-volume shops often check more frequently, since filter loading and operator habits change quickly under heavy production.
Does having an extractor mean a shop meets ventilation requirements?
No, owning an extractor does not by itself show that a shop meets applicable requirements. Regulators and auditors look at hazard assessment, effective capture at the breathing zone, maintenance, and training, so equipment is only one part of the picture.
How do I know if my fume extractor is capturing fume effectively?
Observe the fume plume during normal production and confirm it is drawn into the hood rather than drifting past it. Also measure hood distance from the arc and, where available, compare face velocity readings against the equipment's rated performance.
When should welding shops update their ventilation documentation?
Update the documentation whenever the shop adds a new metal, process, coating, bay, or extractor. A scheduled annual review also helps catch drift between written records and actual conditions on the floor.
Who should be responsible for ventilation records in a fabrication shop?
A named safety lead or facility manager should own the records, with station supervisors contributing routine entries. Clear ownership prevents gaps and makes it easy to show who verified each control and when.